Discontinued lines: having a pipe made from a sample or a part number
- Author
- Alperen Kumru
- First published
- First published:
- Last updated
- Last updated:
- Reading time
- 6 min read
- Category
- OEM numbers and sourcing
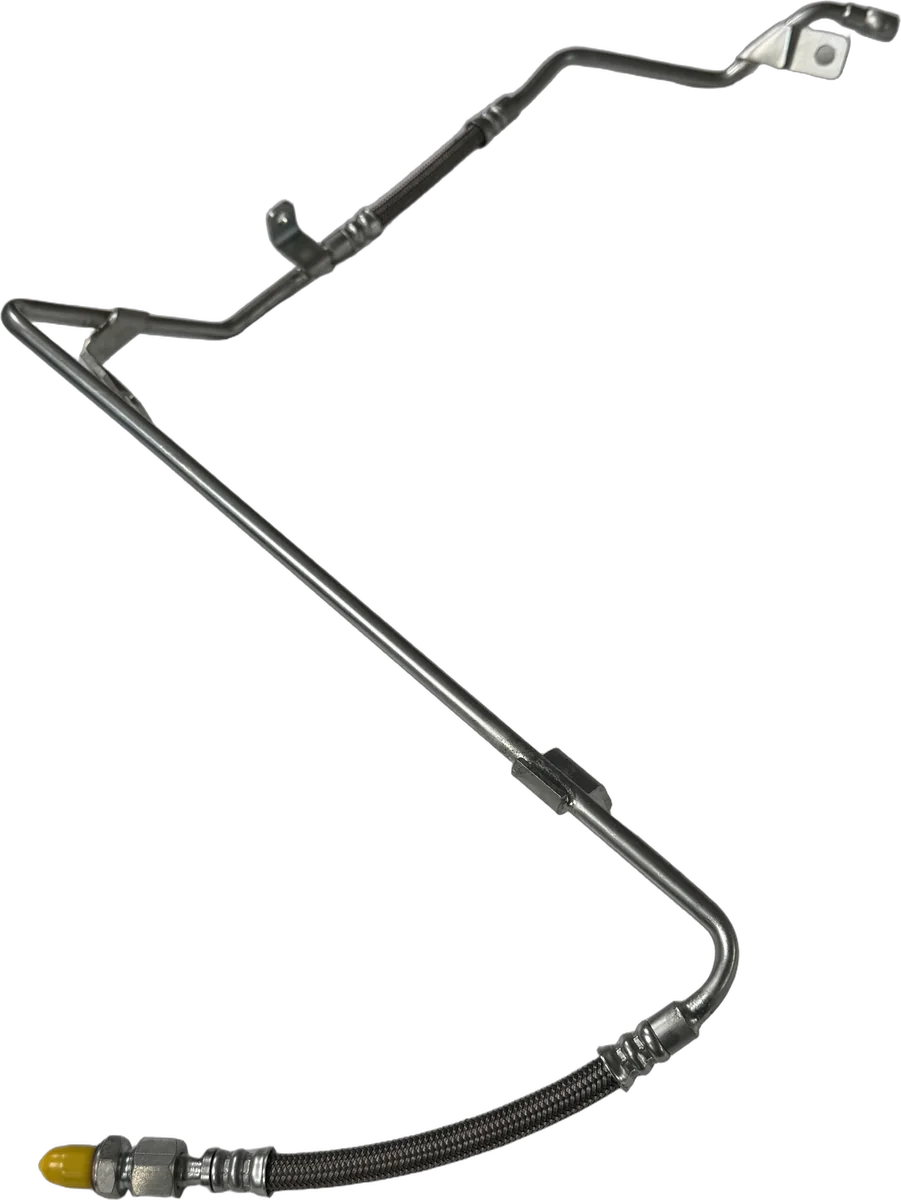
A discontinued injector line, fuel pipe or power steering pipe can be made again from the old pipe, a technical drawing or the part number. Feasibility comes down to four things: tube diameter and wall thickness, the end forms, the nuts and the bends. Tooling and programming are needed even for one piece, so their cost lands on however few pieces are made. The route is the same for an owner after one pipe and for a business that sells parts for classic and vintage vehicles.
Short answer
- What to supply: the old pipe, nuts on and not straightened, or a dimensioned drawing; plus the part number and engine and machine details.
- What decides feasibility: tube size, end form and tooling, the nut, and the radius and angle of each bend.
- Why a minimum quantity: tooling and programming do not depend on quantity; their cost is spread over the batch.
- The first piece: fit it to the vehicle and try it before the batch is approved.
Why does a pipe become unobtainable?
By the one manufacturer’s account we have read, a part becomes unobtainable when stock runs out and only a handful are still wanted. The classic division of a car manufacturer opens a 2018 press release with the words “No longer available”. There, a part that is out of stock or running low is reproduced “using the original tools”, and larger quantities may need new tools. The hard case is the part that very few owners need:
“Producing small batches using new tools would be largely inefficient.”
Classic division of a car manufacturer, press release, 12 February 2018
On a tractor forum, an owner looking for six injector lines writes that two suppliers “told me they are discontinued and they don’t have them in stock”. When his dealer searched the stock of other dealers, two of the six turned up. A part may also have been superseded, not dropped; for Caterpillar, that is covered in our article on part numbers.
What do you give the manufacturer?
To have a pipe made, the manufacturer needs something that carries the tube size, both ends and the shape: the old pipe, a technical drawing, or the part number. The old pipe describes the shape best; the forum owner sent his old set to a diesel shop to have a new one made. We suggest this package:
- Sample. The old pipe as it came off: not straightened, not cut, nuts left on both ends. Say if it is bent or crushed anywhere.
- Drawing. With no usable sample, a dimensioned drawing: tube size, the form of each end, and the position, angle and direction of every bend.
- Number and plate data. The number on the pipe or in the parts book; the model and serial number of engine and machine.
What to measure is in our guide to describing a line with no part number, which also explains why injector line dimensions cannot be approximated. A part number on its own carries no dimensions; it is enough only when the manufacturer already holds the drawing or the measurements behind it. Our sources do not spell this out; it follows from a part number being a name.
What decides whether the job is feasible?
Four things decide whether the pipe can be made: tube diameter and wall thickness, the end form, the nut and the bends. Per a bending-tooling supplier, tooling is specified for the exact tube material, diameter, wall thickness and bend radius; the bend die “has to match the tube’s outer diameter and the specified centerline radius”.
- Diameter and wall thickness. For tight-radius or thin-wall bends, the supplier adds, a mandrel goes inside the tube “to prevent the tube wall from collapsing or wrinkling”. On an injector line the size is also binding: a diesel injection reference book speaks of “prescribed line dimensions that must be strictly observed”.
- End form. A tube-industry journal describes one of the most common end forming machines: clamp dies hold the tube still while “a tool secured to the ram forms the tube’s end”; between its two examples, the only difference is the shape of that tool. On an injector line the end is a sealing cone, which the reference book says “can be shaped from the base material”.
- Nut. In the same book the union nut presses the cone into the fitting to make the seal; some versions add a thrust washer to spread the nut’s force evenly over the cone.
- Bends. Before tooling is specified, the tooling article wants the radius and angle of every bend in the part defined. Nor is tooling interchangeable between makes of bender: “tooling mounting and sizing standards vary between manufacturers”.
On a second tractor forum, someone wanting a 37° flare on 1-1/2 inch tubing writes that nuts and sleeves in that size are available, but “I cannot find ANYONE who can flare that big”. A member replies that his own shop could do it.
Why is there a minimum order quantity?
A minimum order quantity spreads the cost of tooling and programming, incurred even for one piece, over enough pieces. Our sources state no minimum quantity; this is our own inference from what they describe. The classic-parts press release calls producing small batches with new tools largely inefficient. The bending-tooling supplier spells out what wrongly specified tooling costs:
“Getting tooling specification right up front avoids the trial-and-error cost of scrapped tube and machine downtime.”
A bending-tooling supplier, article, 15 June 2026
So the preparation is the same for one pipe as for a batch: without tooling for that diameter and radius, new tooling is needed, and the CNC bender is programmed for that part. Its cost is divided by the number made.
The same inference goes one step further: a batch of the same pipe spreads the set-up cost across the pieces. Made-to-order production therefore suits a business that sells the same part regularly better than a buyer ordering one at a time; suppliers of classic and vintage vehicle parts are the obvious case.
What do you check when the first piece arrives?
The first piece is fitted to the vehicle and tried; size and fit show up there. The classic-parts press release says the same: “Accuracy in terms of size and fit is ensured by performing tests with the part installed.” We suggest approving the rest of the batch only after that.
For an injector line: compare the new line with the old one bend for bend, start both nuts by hand, and see that each end sits on its seat without being held and that the clamps go back on. The sequence and the reasons are in our article on why injector lines crack.
What do we work from, and in what quantity?
RSS Kumru manufactures to an OEM number, a technical drawing or a sample; in some cases without a physical sample, from technical information or a drawing alone. For a special run made from a sample or a number, the minimum order quantity is usually between 50 and 100 pieces; it varies with the kind, type and difficulty of the product.
What should you do with a discontinued pipe?
- Confirm the number. Has it been superseded? Has the dealer searched other dealers’ stock?
- Keep the old pipe. Even cracked, it carries the dimensions and the shape.
- Talk about quantity. Ask for the minimum quantity and whether new tooling is needed.
- Fit and try the first piece. Approve the rest of the batch only after that.
Sources
- Porsche Newsroom (Porsche AG), “Porsche Classic supplies classic parts from a 3D printer”, press release, 12 February 2018; reproducing parts that have run out, new tools for small batches, testing with the part installed.
- Tube Form Solutions, “CNC Tube Bender Tooling: Components, Specification, and Turnkey Solutions”, article by a bending-tooling supplier, 15 June 2026; bend dies, mandrels, specifying tooling to the tube, the scrap and downtime cost of wrong tooling.
- Bosch / Springer, “Diesel Engine Management: Systems and Components (ed. Konrad Reif), pp. 168-170”, reference book, 2014; pp. 168-170, read in Google Books partial view; sealing cone, union nut, thrust washer and the rule on line dimensions.
- The Fabricator / The Tube & Pipe Journal, “Putting a few end forming basics to work”, trade journal article, 9 March 2009; forming tube ends, the ram-type end former and its tooling.
- OrangeTractorTalks, “Discontinued Kubota Injector Lines”, forum thread, 31 October to 8 November 2024; one owner's account of discontinued injector lines, cited as a field example.
- TractorByNet, “DIY hydraulic hard lines?”, forum thread, 15 April 2013 to 10 May 2019; a question about flaring large tubing and the reply, cited as a field example.
Sources were checked again on October 9, 2026.
RSS Kumru Automotive
RSS Kumru Automotive was founded in 1990 and specialises in hydraulic systems and fluid management. Our range includes injector lines, fuel and oil lines, hoses and fittings.
Brand names and OEM reference numbers are used for identification and compatibility information only.